Service 01Prototype to Production
3D Printing Services
FDM 3D printing in engineering plastics—from validating a concept to ready-to-use parts, with controlled finishing and inspection.
How We Work
DFAM → Build → Finish
Loading…
Manufacturing services
Functional prototypes, tooling and production parts in FDM, from one part. We choose the material, orientation and finish for what your part has to do.
Upload your file and quote your printed part
Upload your 3D filesDrag your files here
STEP, STP, STL, 3MF, DXF, DWG · Drawings as PDF or photo · Start without an account
Confidential files. Your design and intellectual property stay yours.
No CAD file? Request a manual quote
We 3D print your part fast without giving up fit, function, or reliability. We review your geometry and tell you whether FDM or CNC machining fits what your part needs: strength, looks, and quantity.
When we quote, we review your design for printing (DFAM): orientation, supports, minimum features, holes/threads, and visible zones. That means fewer failed prints, better dimensions, and no surprises after finishing.
From one part to production lots, we keep your parts repeatable with clear specs, controlled finishing, and inspection focused on what matters most on your part.
From uploading your CAD to getting your parts—fast and straightforward.
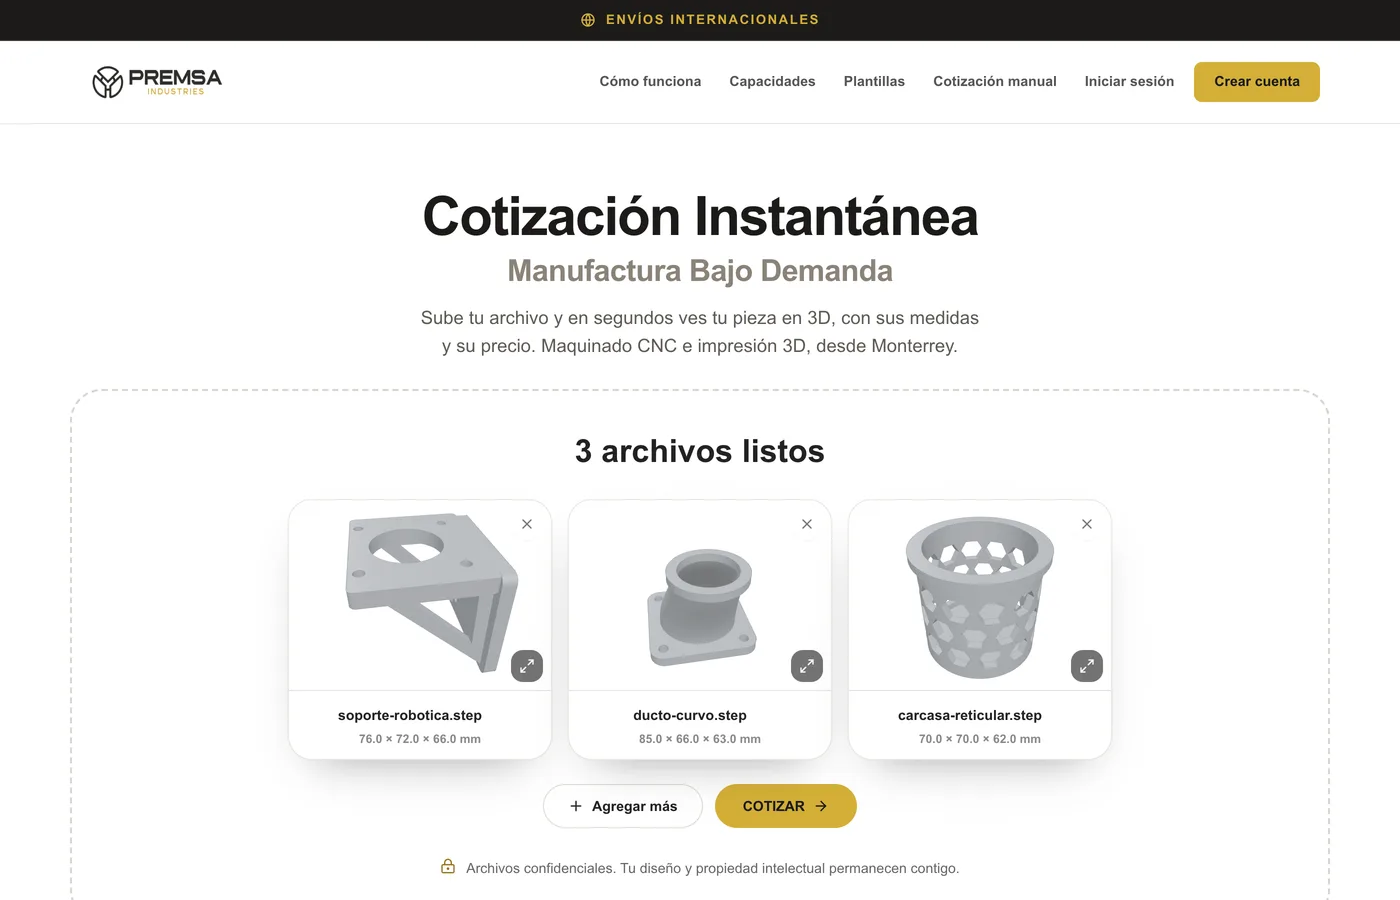
Additive manufacturing (AM) produces parts by building material layer-by-layer rather than removing material (machining) or forming it in a mold. This makes AM ideal for fast iteration, complex geometry, internal channels, lightweight lattices, and consolidated assemblies.
A good printed part depends on process physics (layering, temperature), material behavior, and finishing. DFAM aligns geometry, orientation, supports, and critical surfaces so it comes out right.
1. Requirements & DFAM
We confirm prototype vs production, loads, visible zones, and critical dimensions. We check minimum features, supports, and orientation effects.
2. Process Selection
We pick what meets your requirements: FDM for tough thermoplastics, fiber-filled if you need more stiffness, or CNC machining if your part needs metal or tight tolerances.
3. Build Preparation
We set orientation, bed layout, supports, and parameters to balance surface quality, strength direction, and dimensional stability.
4. Printing / Building
We print with controlled parameters and watch quality during the print.
5. Post-Processing
Supports removed and parts cleaned as needed.
6. Finishing (Optional)
Bead blast, dye, paint, machining of critical faces, thread inserts, or sealing surfaces depending on requirements.
7. Inspection & Documentation
Critical dimensions inspected per plan; first-article report when you ask for it.
8. Packaging & Delivery
Parts packed to protect surfaces and geometry, shipped with any required documentation.
Print when the shape is complicated
Internal channels, ribs, pockets and organic shapes that would take hours on a mill cost about the same as a simple shape when printed.
Print when you need a few parts fast
No mold and no tooling: from 1 to hundreds of parts, with the price per part dropping as you order more.
Machine when you need metal or tight tolerances
Bearing fits, threads that get tightened over and over, or load-bearing parts: that's CNC machining in aluminum, steel or stainless.
Compare with real prices
A ribbed bracket printed in PETG is US$14 for one part and US$8.10 at 100 parts. A similar bracket milled in 6061 aluminum is US$72 and US$28.14. If plastic can take the load, printing is much cheaper.
Combine both
We print the part and machine only what's critical: the bearing bore, the seating face or the thread. You pay for machining only where it's needed.
Use it while the mold is on its way
3D printing covers your parts while your mold or tooling is being made, without stopping the line.
3D printing focused on detail, function, and repeatability.Every part is reviewed for design, material, finish, and inspection.
FDM 3D printing in engineering plastics—from validating a concept to ready-to-use parts, with controlled finishing and inspection.
How We Work
DFAM → Build → Finish
Layer-based thermoplastic extrusion for functional prototypes, fixtures, housings, and engineering components requiring strength and cost efficiency.
How We Work
DFAM → Build → Finish
Prototypes printed fast to validate fit, form, and function, so you can decide sooner.
How We Work
DFAM → Build → Finish
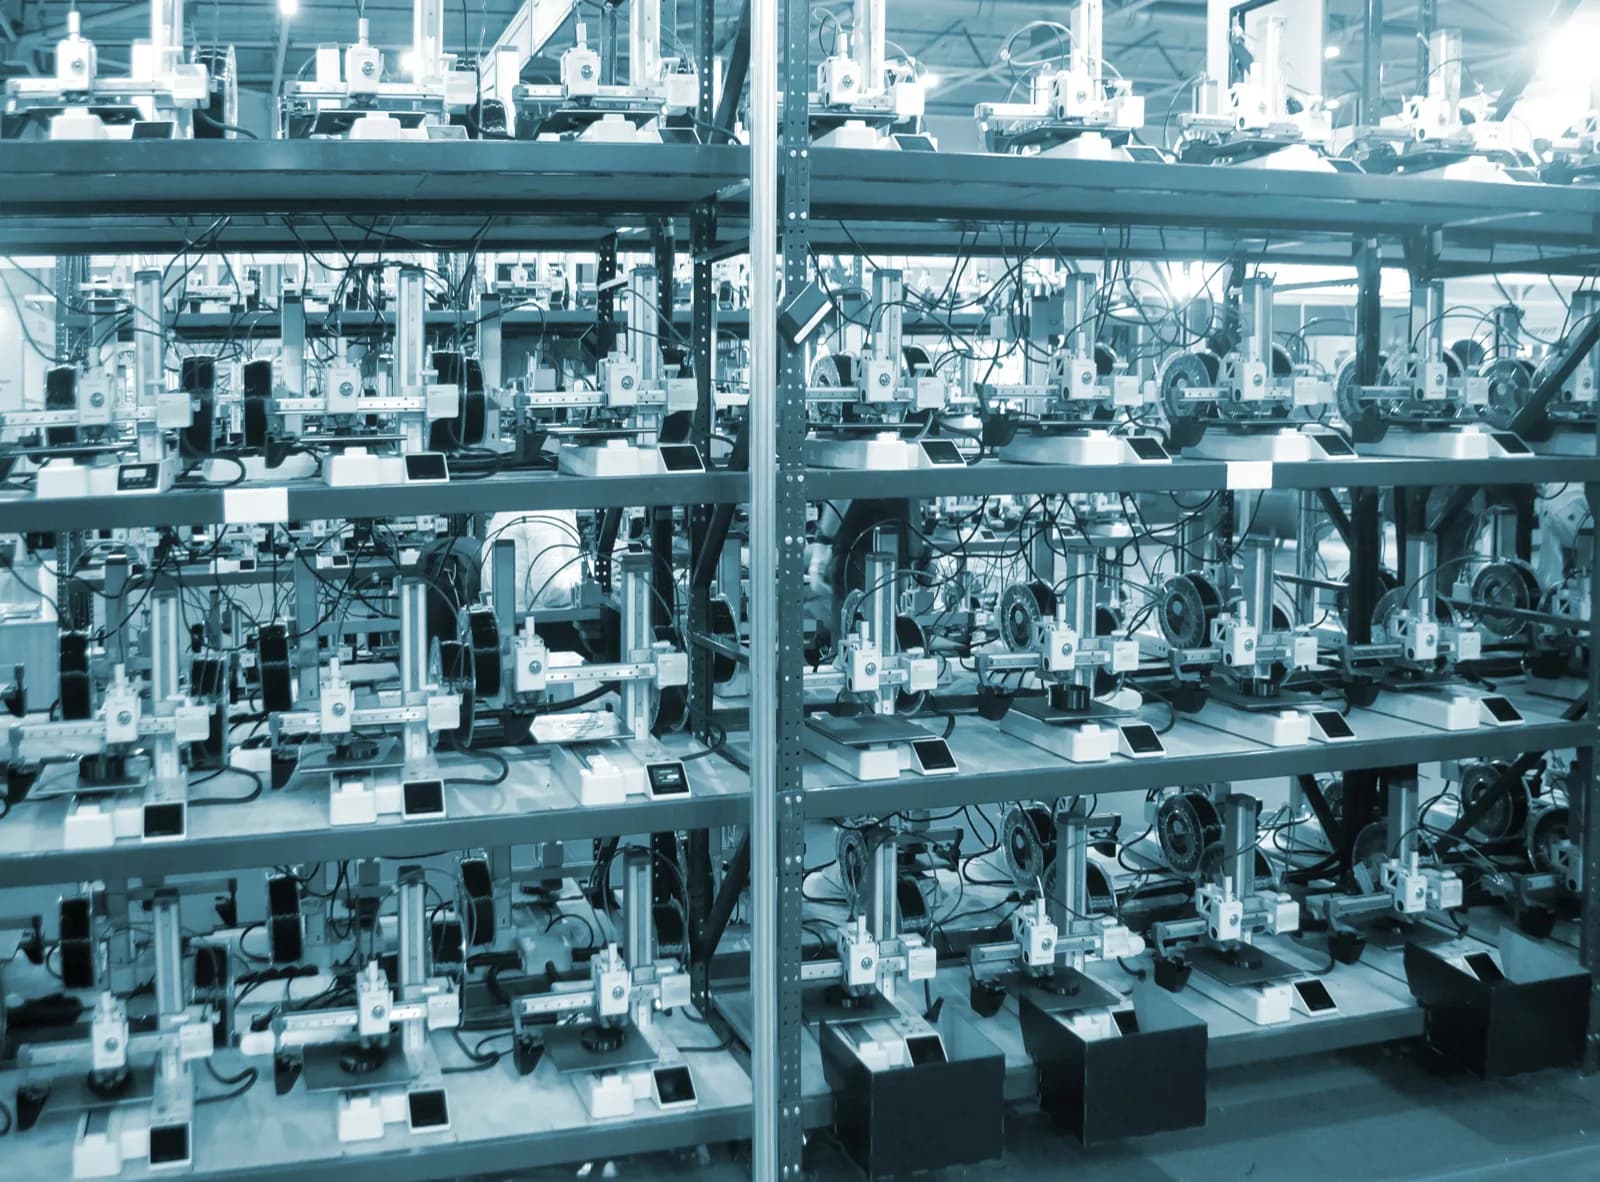
Runs of printed parts with controlled parameters, standard finishing, and defined inspection, ready for end use.
How We Work
DFAM → Build → Finish
From one part to repeatable production runs, depending on the material.
Prototype → Production
Print quality of your choice plus finishing options to improve the surface.
Based on print quality
Engineering thermoplastics, fiber-filled or flexible, based on function and environment; metal we CNC machine.
Engineering Plastics
Upload your CAD and we'll tell you whether FDM or CNC machining fits better based on geometry, requirements, and quantity.
3D printing tolerances depend on material, part size, orientation, and post-processing. Clear requirements let us balance cost, risk, and inspection.
| Category | Technical Description | Typical Notes |
|---|---|---|
| Dimensional Expectations | Dimensional results vary with process and part envelope. Critical features often benefit from design allowances and post-machining of datums or mating interfaces. | Call out CTQs; consider machining allowances for tight fits and sealing surfaces. |
| Surface Finish & Layer Lines | Layering can create visible texture depending on process and orientation. Finishing steps (bead blast, tumbling, sanding, coating) can improve cosmetics. | Define cosmetic zones; allow non-cosmetic surfaces where supports or texture may exist. |
| Anisotropy & Orientation Effects | Strength and stiffness can vary by build direction. Orientation impacts surface quality, support marks, and dimensional outcomes. | Share load directions so we can orient parts for performance, not just appearance. |
| Inspection & Reporting | Inspection can range from sampling key features to detailed first-article reports, depending on what your part needs. | We provide first-article reports and ongoing sampling when you ask for them. |
| Process Control & Repeatability | Repeatability improves with stable parameters, consistent post-processing, and controlled finishing—especially for production runs. | For production, define finishing steps and acceptance criteria (color, texture, marks). |
Not all plastics hold up the same. Choose by **what your part has to withstand**: heat, impact, sun or load. If you're not sure, upload it and we'll recommend one.
Temperatures are approximate heat-deflection values under light load. Real strength also depends on orientation and infill.
An FDM part comes off the printer with visible layers. Depending on where it's used, it stays that way or gets a finish.
DFAM reduces print risk and improves yield. These guidelines focus on orientation, supports, minimum features, and post-processing realities.
| Design Feature | Technical Recommendation |
|---|---|
| Orientation & Support Strategy | Orient parts to protect cosmetic faces, reduce supports, and align strength direction with load paths. Support contact areas should be placed on non-cosmetic zones where possible. |
| Wall Thickness & Minimum Features | Maintain adequate wall thickness for stability and handling. Avoid long thin walls without ribs; use fillets and gradual transitions to reduce distortion risk. |
| Holes, Threads & Critical Fits | Holes often print undersized; plan to drill/ream if needed. For threads, consider inserts or machining for durability and precise fit. |
| Snap Fits, Flexures & Compliance | Design compliant features with material and build-direction behavior in mind. Validate flexure life and allow iterations for performance tuning. |
| Surface Zones & Cosmetic Control | Define A/B/C surfaces and acceptance criteria (layer lines, support marks, texture). Cosmetic clarity prevents misalignment during finishing. |
| Designing for Post-Processing | Plan access for cleaning and finishing steps. Add machining allowances on datums and sealing faces if tolerances are tight. |
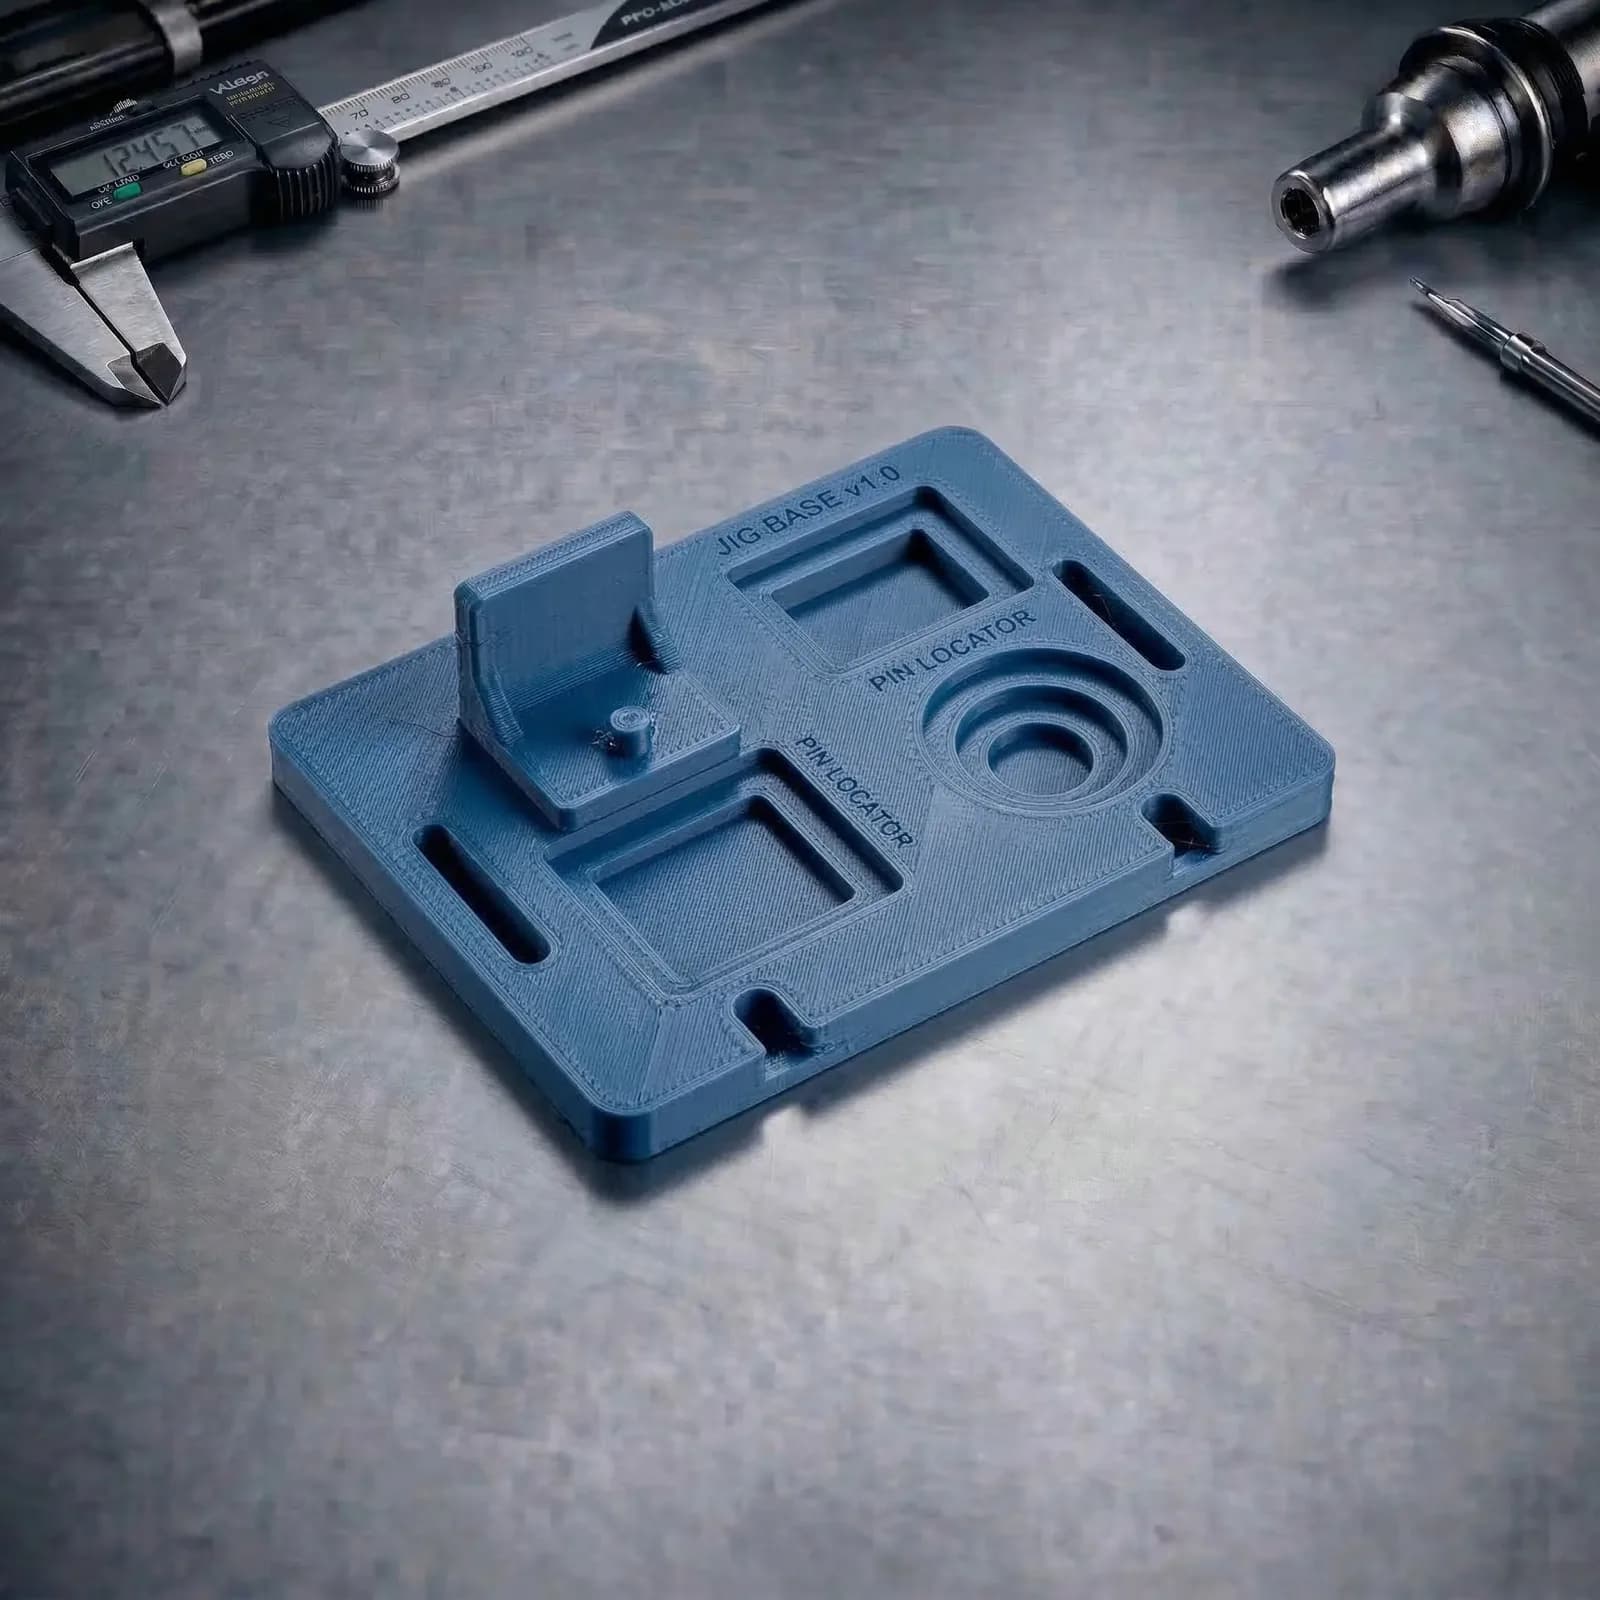
Custom fixtures, nests, drill guides, and assembly aids—optimized for fast iteration and ergonomic improvements without tooling cost.
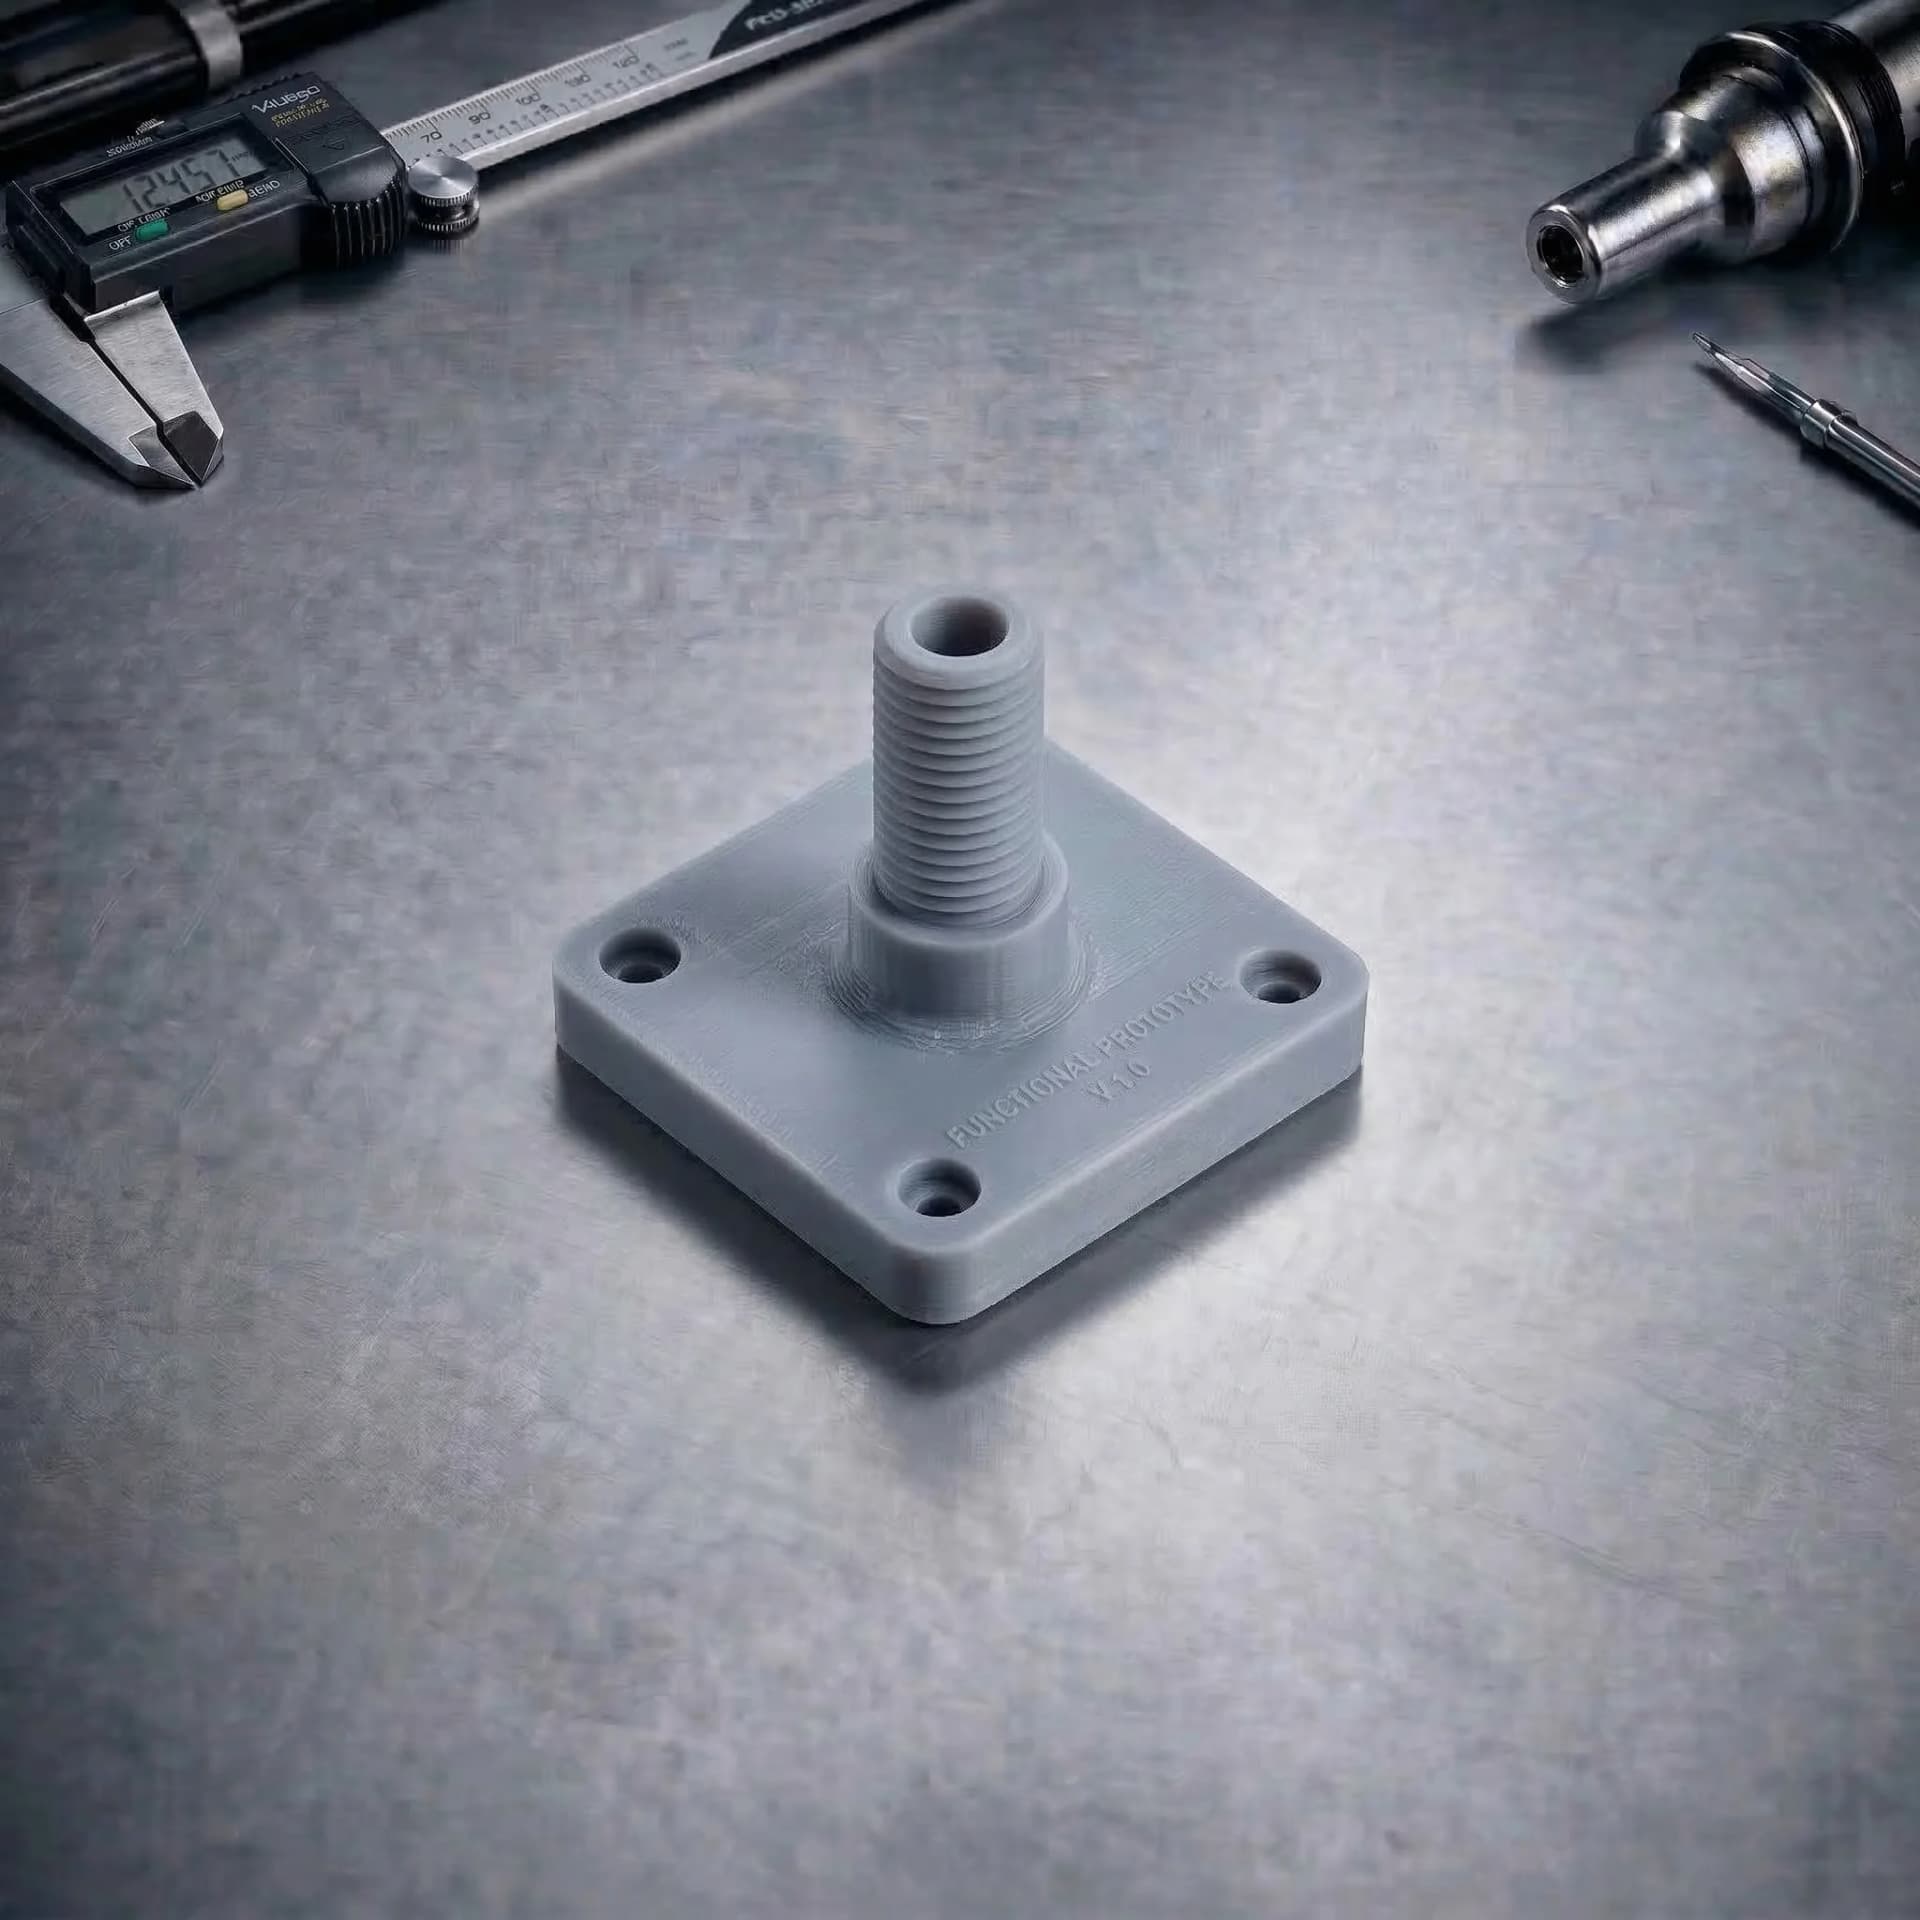
Rapid prototypes to validate assemblies, interfaces, and design intent; we pick the material based on the decision you need to make.
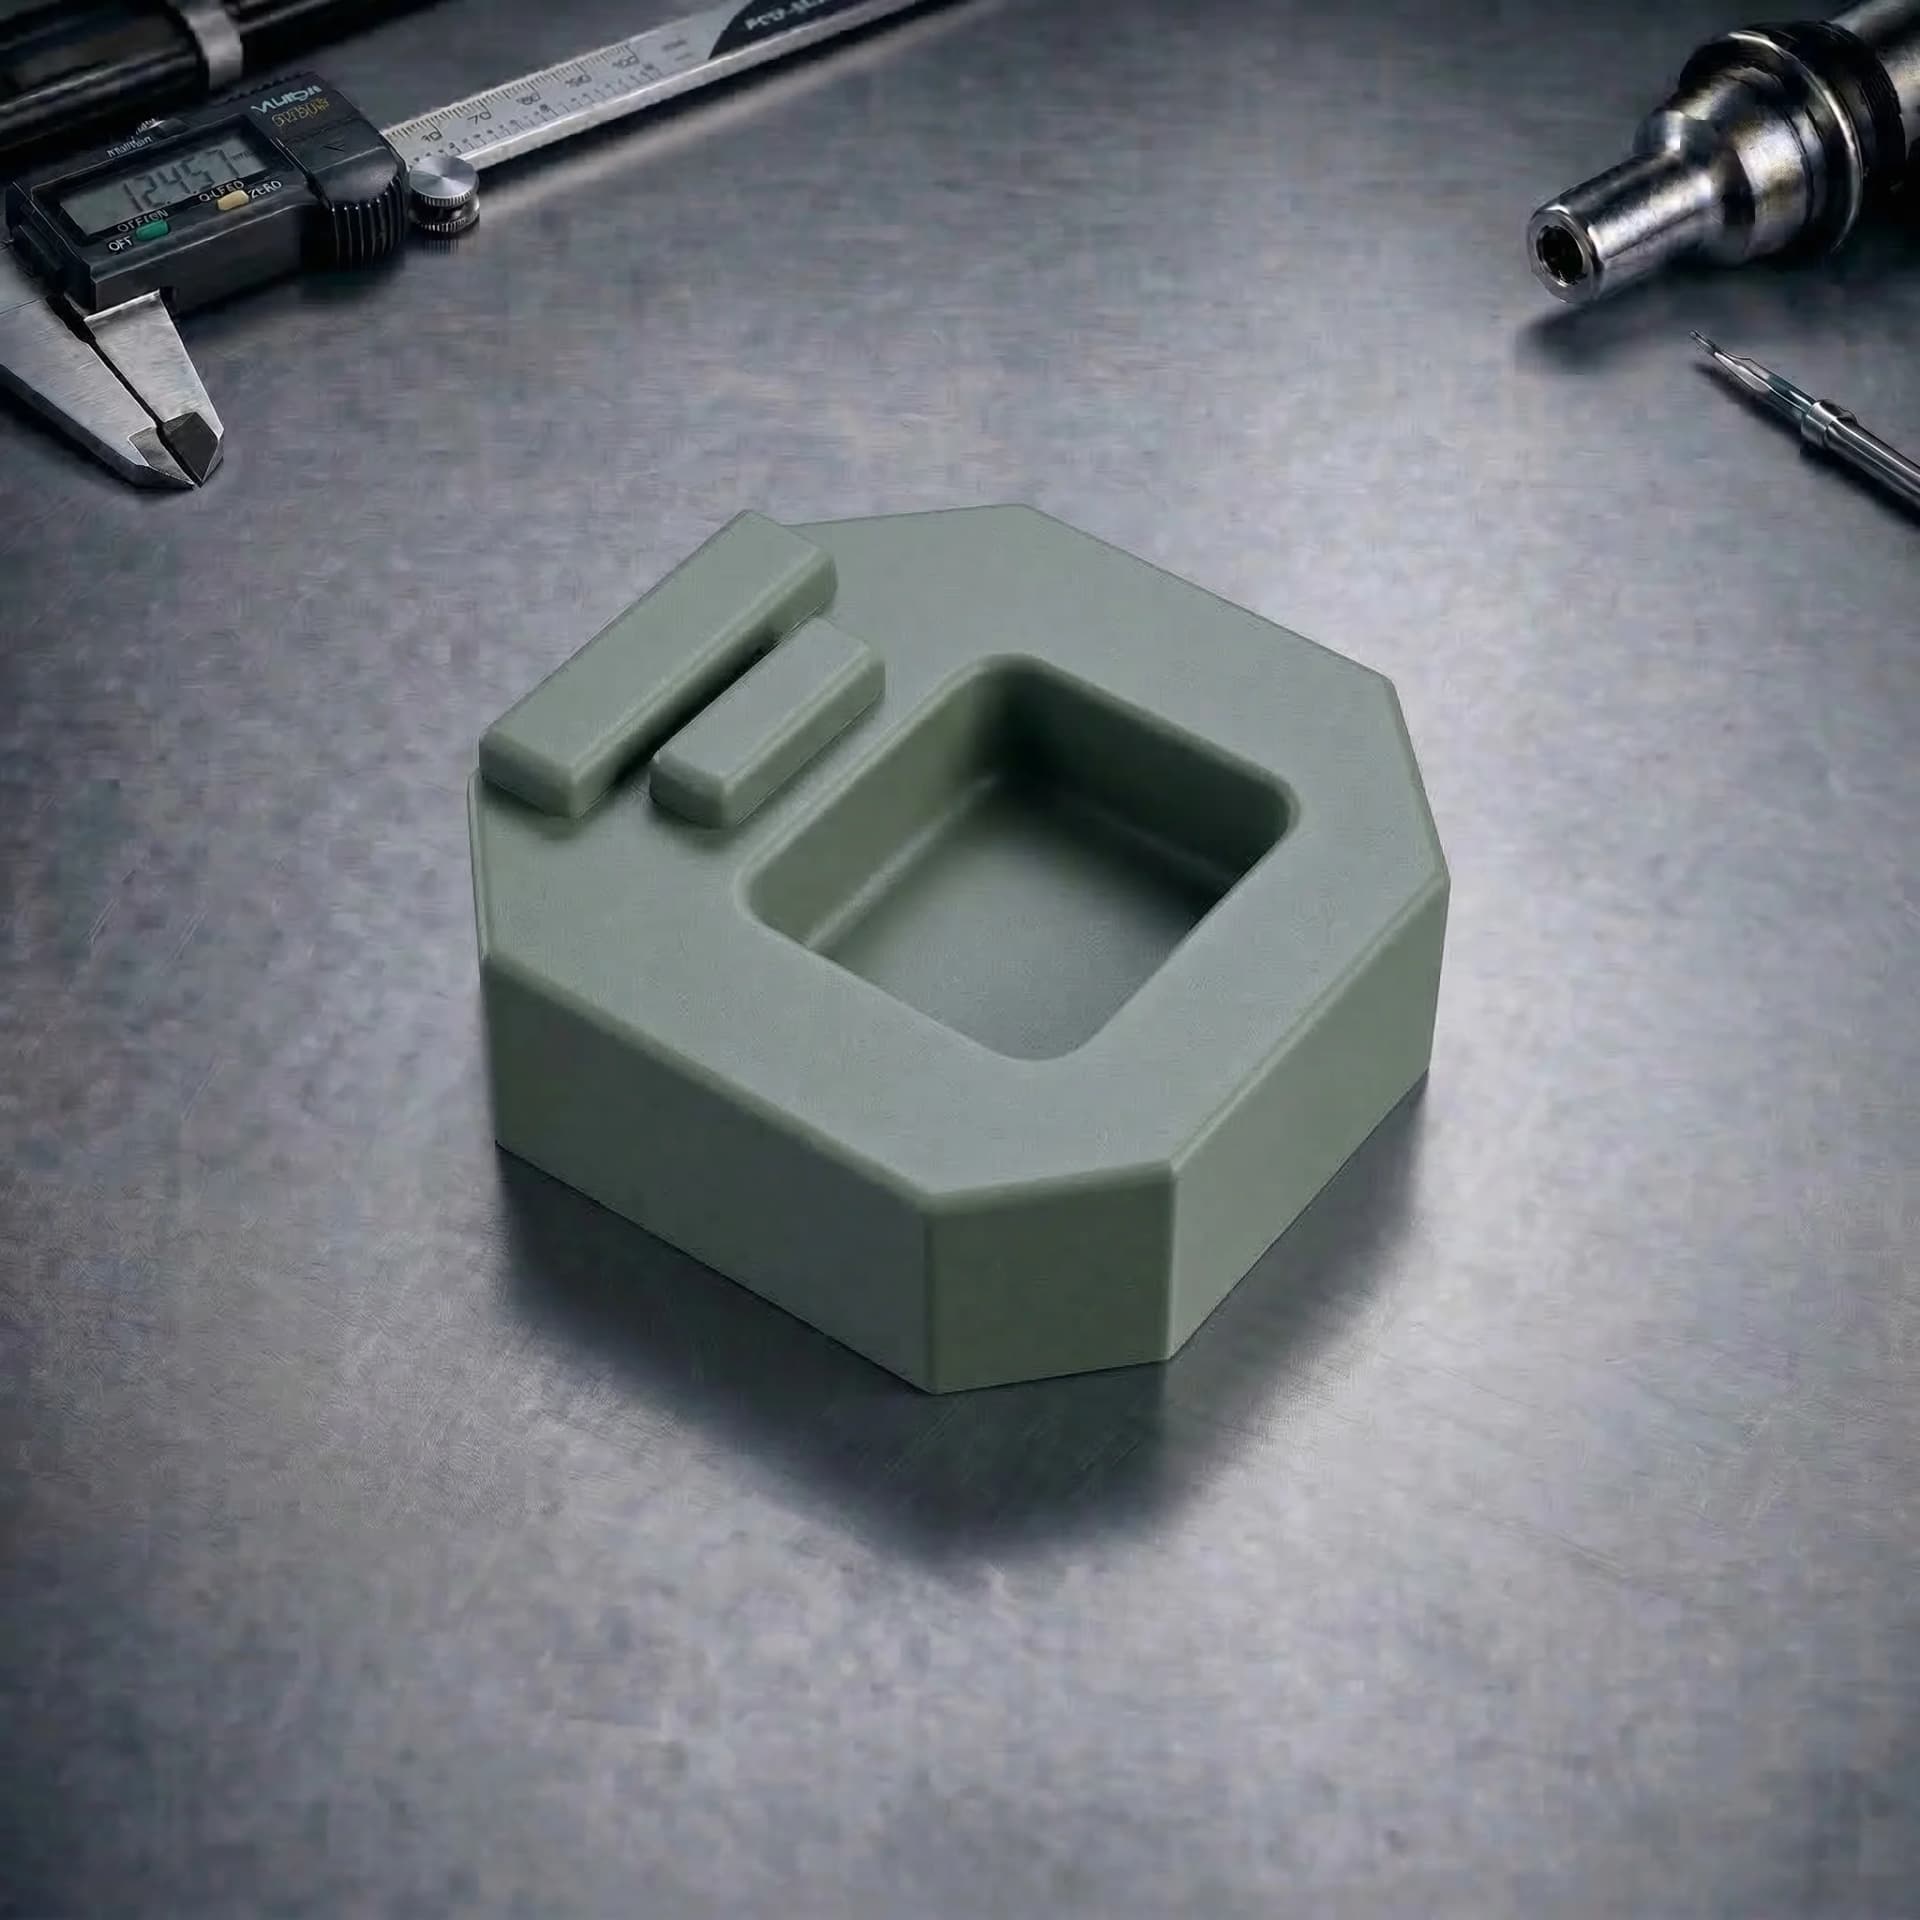
End-use FDM parts in engineering plastics when tooling isn't justified or every part is different.
Fixtures, guards, brackets, housings, and service parts with fast turnaround and iterative improvement cycles.
Enclosures, sensor mounts, cable management, and assembly-ready parts where iteration speed and fit matter.

Complex geometries, lightweighting concepts, and specialized prototypes—requirements-driven process selection and finishing.
Additive manufacturing builds a part layer by layer instead of removing material. At PREMSA we do it in FDM with engineering plastics, and it pays off when the part has shapes that would be expensive to machine, when you need a few parts without paying for a mold, or when you want to test a design this week instead of next month.
What makes it work isn't the printer, it's choosing well: the material for the heat and load it will see, the orientation so the part is strong where it works, and the finish it needs. We review that with your file before printing.
And because we also machine, you don't have to guess the process: if your part comes out better or cheaper with CNC, we tell you. Upload your file and order from one part.
PREMSA ecosystem
We make parts in Monterrey for anyone who needs one, shipping across Mexico and worldwide. We print in FDM with ISO 2768 tolerances, engineering materials, and prototype-to-production routes, and we CNC machine when you need metal. Use the technical references below and quote online with STEP or STL files.
Full additive portfolio overview.
View serviceRapid prototypes and design validation.
View serviceRepeatable additive production.
View serviceFused deposition modeling for functional prototypes.
View serviceGeneral linear and geometric tolerances for machined and formed features.
View chartHole diameters for metric, UNC, UNF, and NPT threads.
Open toolNumber, letter, and fractional drill diameters.
View chart